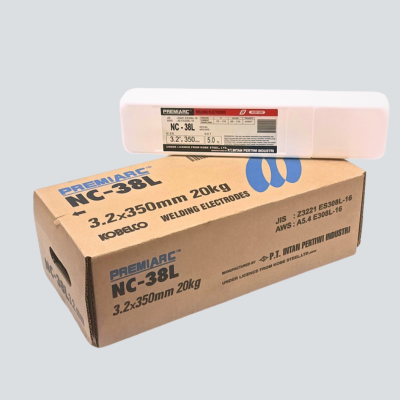
NC-38L Welding Electrode, E308L-16: Flexible electrode for welding 304L and 304 stainless steel in all positions, suitable for low to high temperatures, with low carbon deposit metal (0.034%) and composition 18%Cr – 8%Ni.
With advanced features and precise specifications, the NC-38L and E308L-16 are ideal solutions for welding stainless steel that requires high durability, flexibility, and industrial-grade quality.
AWS A5.4 E308L-16
NC-38L, E308L-16 welding electrode is a welding electrode specifically designed for welding applications on 304L and 304 stainless steel types.
This electrode has high flexibility, so it can be used in all welding positions, whether flat, upright, inverted, or horizontal.
| Parameters | Description |
|---|---|
| Product Name | Welding Electrode NC-38L |
| Brand | KOBELCO |
| Electrode Type | Welding Electrodes for Stainless Steel |
| Welding Electrode Size | 2.0mm, 2.6mm, 3.2mm, 4.0mm and 5.0mm |
| Weight Per Packaging | 20 Kg |
| AWS Standard | AWS A5.4 E308L-16 |
| Re-Drying Conditions | 150–200°C for 0.5–1 hour |
| Identification Color | Red (1st Red) |
| Polarity | AC, DCEP |
The following are the typical mechanical properties of NC-38L weld metal, demonstrating the strength, ductility, and toughness of the weld in accordance with KOBELCO specifications.
| Parameters | Typical | Guaranty |
|---|---|---|
| Yield Strength | 410 MPa | – |
| Tensile Strength | 580 MPa | ≥ 518 MPa |
| Elongation | 48% | ≥ 30% |
| Impact Value (0°C) | 78 J | – |
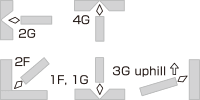
The NC-38L can be used in various welding positions, making it suitable for fabrication and installation work that requires flexibility in the field.
Use the following recommended welding current ranges to achieve stable welds, optimal penetration, and consistent joint quality.
| Diameter (mm) | 1F, 1G, 2F, 2G | 3G Uphill, 4G |
|---|---|---|
| 2.0 | 50–75 A | 45–65 A |
| 2.6 | 75–95 A | 70–90 A |
| 3.2 | 85–120 A | 80–115 A |
| 4.0 | 110–160 A | 90–140 A |
| 5.0 | 150–200 A | – |
The chemical composition of the NC-38L weld metal is designed to provide good corrosion resistance, structural stability, and mechanical properties that meet the AWS A5.4 E308L-16 standard.
| Element | Typical | Standard Limit |
|---|---|---|
| C | 0.03 | ≤ 0.04 |
| Si | 0.38 | ≤ 1.00 |
| Mn | 1.50 | 0.50–2.50 |
| P | 0.02 | ≤ 0.04 |
| S | < 0.01 | ≤ 0.03 |
| Ni | 9.60 | 9.00–11.00 |
| Cr | 20.30 | 18.00–21.00 |
| Mo | 0.14 | ≤ 0.75 |
| Cu | 0.05 | ≤ 0.75 |
Note: The single limit value (≤) indicates the maximum permissible level according to the standard.
The following packaging information facilitates planning for the storage, shipping, and usage requirements of NC-38L welding electrodes.
| Diameter (mm) | Length (mm) | kg/Pack | kg/Carton | g/bar | Carton Dimensions (mm) |
|---|---|---|---|---|---|
| 2.0 | 250 | 2 | 20 | 11 | 300W × 125H × 280L |
| 2.6 | 300 | 2 | 20 | 20 | 300W × 100H × 330L |
| 3.2 | 350 | 5 | 20 | 36 | 175W × 115H × 380L |
| 4.0 | 350 | 5 | 20 | 55 | 175W × 130H × 380L |
| 5.0 | 350 | 5 | 20 | 82 | 175W × 130H × 380L |
Order KOBELCO NC-38L welding electrode now through the available contacts.
ISO 9001:2015
ISO 14001:2015
© 2026, PT. Intan Pertiwi Industri | All Rights Reserved.