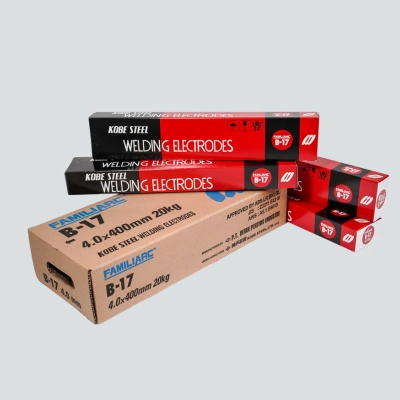
Welding Electrode B-17 is a high-quality welding solution for low to medium carbon steel. Ideal for construction, fabrication, and repair. Flexible, corrosion resistant, and easy to use.
AWS A5.1 E6019, JIS D4301
Welding Electrode B-17 is a reliable solution for low to medium carbon steel welding needs. Designed with modern technology, this welding electrode offers exceptional performance in a wide range of industrial applications, from building construction and shipbuilding to metal fabrication and structural repair.
| Parameters | Description |
|---|---|
| Product Name | Welding Electrode B-17 |
| Brand | KOBELCO |
| Classification | AWS A5.1 E6019 |
| Main Application | Welding electrodes for carbon steel |
| Welding Electrode Size | 2.6 mm, 3.2 mm, 4.0 mm |
| Welding Process | SMAW (Shielded Metal Arc Welding) |
| Weight per Package | 20 Kg |
| Polarity | AC, DCEP, DCEN |
| Identification Color | Yellow (1st Yellow) |
| Redrying Conditions | 70–100°C for 0.5–1 hour |
Welding Electrode B-17 offers excellent performance for welding low to medium carbon steel, with high flexibility in various welding positions such as flat, vertical, and overhead.
With a flux core that protects the weld pool from air contamination, this electrode produces strong, smooth, dense welds with minimal spatter, and provides good corrosion resistance.
Welding Electrode B-17 is also compatible with FCAW or MIG/MAG welding machines, making it an efficient and reliable choice for construction, metal fabrication, shipbuilding, and structural repair applications.
Mechanical properties of all metals being welded
| Parameters | Typical Value (AC) | Minimum Standards (Guarantees) |
|---|---|---|
| 0.2% Yield Strength | 420 MPa | ≥ 331 MPa |
| Tensile Strength | 470 MPa | ≥ 414 MPa |
| Elongation (Elongation, 4d) | 31% | ≥ 22% |
| Charpy V-notch impact value (-18°C) | 80 J | ≥ 27 J |
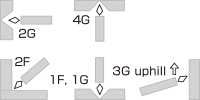
KOBELCO B-17 welding elctrode supports various welding positions, offering flexibility in both fabrication processes and construction work.
Recommended welding positions include:
| Electrode Diameter (mm) | 1F, 1G, 2F, 2G (Ampere) | 3G Vertical Up & 4G (Ampere) |
|---|---|---|
| 2.6 mm | 50 – 85 A | 40 – 70 A |
| 3.2 mm | 80 – 130 A | 60 – 110 A |
| 4.0 mm | 120 – 180 A | 100 – 150 A |
| 5.0 mm | 170 – 250 A | 130 – 200 A |
| 6.0 mm | 240 – 310 A | – |
| Classification | Approval |
|---|---|
| ABS (American Bureau of Shipping) | 3 |
| LR (Lloyd’s Register) | 3m |
| DNV (Det Norske Veritas) | 3 |
| BV (Bureau Veritas) | 3 |
| NK (Nippon Kaiji Kyokai) | KMW3 |
| CR (China Classification Society) | 3 |
| Chemistry Value | Typical | Guaranty* |
| C | 0.09 | 0.20 |
| Si | 0.08 | 1.00 |
| Mn | 0.60 | 1.20 |
| P | 0.012 | 0.035 |
| S | 0.006 | 0.035 |
| Ni | 0.01 | 0.30 |
| Cr | 0.02 | 0.20 |
| Mo | < 0.01 | 0.30 |
| V | < 0.01 | 0.08 |
Note : (*) Single values is maximum.
| Diameter (mm) | Length (mm) | Weight/pack (kg) |
|---|---|---|
| 2.6 | 350 | 5 |
| 3.2 | 350 | 5 |
| 4.0 | 400 | 5 |
| 5.0 | 400 | 5 |
| 6.0 | 450 | 5 |
Additional information:
All sizes are packed in 20 kg/carton.
| Diameter (mm) | Weight/piece (g) | Carton Size (mm) |
|---|---|---|
| 2.6 | 19 | 170W × 100H × 380L |
| 3.2 | 31 | 170W × 105H × 380L |
| 4.0 | 57 | 170W × 95H × 430L |
| 5.0 | 85 | 170W × 100H × 430L |
| 6.0 | 154 | 170W × 95H × 480L |
Dry the electrodes again at a temperature of 70°C – 100°C for 30 – 60 minutes before use.
Use the recommended welding parameters where X-ray inspection is emphasized in structural welding applications.
Keep the arc length as short as possible.
Use the back step method or light the arc on a small steel plate specially prepared for this purpose to prevent air pockets from forming when starting welding.
Use a windshield when there are strong winds.
ISO 9001:2015
ISO 14001:2015
© 2026, PT. Intan Pertiwi Industri | All Rights Reserved.