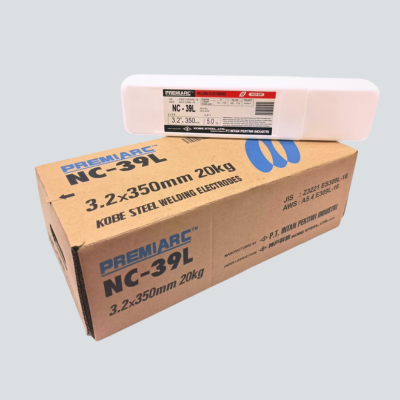
NC-39L welding electrode, E309L-16 – Multipurpose welding electrode for joining carbon steel to inox steel. Suitable for all positions with AC/DC polarity.
AWS A5.4 E309L-16
The NC-39L (E309L-16) electrode is specially designed for welding carbon steel to stainless steel. With a low carbon content (0.030%), this electrode is ideal for buffer coating and capping applications.
Compatible with AC and DC polarity, and supports all welding positions. High-quality weld results with a composition of 22%Cr – 12%Ni.
| Parameters | Description |
|---|---|
| Product Name | Welding Electrode NC-39L |
| Brand | KOBELCO |
| Electrode Type | Welding Electrodes for Stainless Steel |
| Welding Electrode Size | 2.0mm, 2.6mm, 3.2mm, 4.0mm and 5.0mm |
| Weight Per Packaging | 20 Kg |
| AWS Standard | AWS A5.4 E309L-16 |
| Re-Drying Conditions | 150–200°C for 0.5–1 hour |
| Identification Color | 1st Yellow green, 2nd Blue white |
| Polarity | AC, DCEP |
NC-39L, E309L-16
Mechanical properties of all metals being welded
| Parameters | Typical Value (AC) | Guaranty |
|---|---|---|
| 0.2% Yield Strength (YS) | 410 MPa | – |
| Tensile Strength (TS) | 560 MPa | Min. 518 MPa |
| Elongation (EL) on 4D | 42% | Min. 30% |
| Impact Value at 0°C (IV) | 67 J | – |
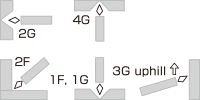
NC-39L can be used in various welding positions, ranging from flat to vertical-up and overhead.
| Diameter (mm) | 1F, 1G, 2F, 2G | 3G Vertical Uplink, 4G |
|---|---|---|
| 2.0 | 50–75 A | 45–65 A |
| 2.6 | 75–95 A | 70–90 A |
| 3.2 | 85–120 A | 80–115 A |
| 4.0 | 110–160 A | 90–140 A |
| 5.0 | 150–200 A | – |
Chemical composition of all welded metals (mass %)
| Element | Typical Value (AC) | Guaranteeᵃ |
|---|---|---|
| C | 0.04 | Max. 0.04 |
| Si | 0.42 | Max. 1.00 |
| Mn | 1.6 | 0.5–2.5 |
| P | 0.03 | Max. 0.04 |
| S | <0.01 | Max. 0.03 |
| Ni | 13.3 | 12.0–14.0 |
| Cr | 23.8 | 22.0–25.0 |
| Mo | 0.18 | Max. 0.75 |
| Cu | 0.09 | Max. 0.75 |
Note: ᵃ The single value represents the maximum limit.
| Diameter (mm) | Packaging Details | Carton Size (mm) |
|---|---|---|
| 2.0 | Length: 250 mm; 2 kg/pack; 20 kg/carton; 11 g/stick | 300W × 125H × 280L |
| 2.6 | Length: 300 mm; 2 kg/pack; 20 kg/carton; 20 g/stick | 300W × 95H × 330L |
| 3.2 | Length: 350 mm; 5 kg/pack; 20 kg/carton; 36 g/stick | 175W × 125H × 380L |
| 4.0 | Length: 350 mm; 5 kg/pack; 20 kg/carton; 55 g/stick | 175W × 115H × 380L |
| 5.0 | Length: 350 mm; 5 kg/pack; 20 kg/carton; 82 g/piece | 175W × 115H × 380L |
| Certification | Approval |
|---|---|
| ABS | MG (AWS A5.4 E309L-16) |
| LR | SS/CMn m (Komposisi Kimia) |
| DNV | VL309L, MG |
| BV | UP (E309L-16) |
| NK | KD309L |
Order NC-39L welding electrode now through the available contact services.
ISO 9001:2015
ISO 14001:2015
© 2026, PT. Intan Pertiwi Industri | All Rights Reserved.