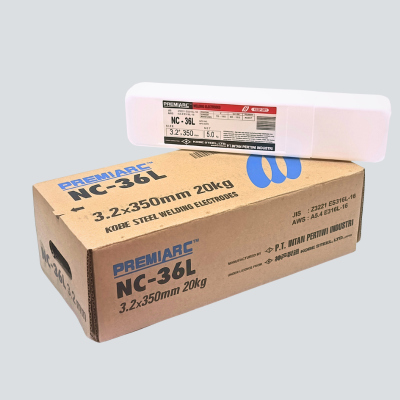
NC-36L welding electrode Kobe Steel E316L-16 for welding 316L stainless steel. Suitable for all positions with AC/DC-EP polarity. Low carbon content (0.023%) and composition of 18%Cr-12%Ni-Mo.
AWS A5.4 E316L-16
KOBE Steel NC-36L, AWS A5.4 E316L-16 welding electrode is a high-quality welding electrode for 316L stainless steel. Designed for all-position welding with AC and DC-EP polarities.
Having a low carbon content (0.023%) and a chemical composition of 18% Chromium, 12% Nickel, and Molybdenum, makes it an ideal choice of welding electrode for industrial applications requiring superior corrosion resistance and mechanical strength.
| Parameters | Description |
|---|---|
| Product Name | Welding Electrode NC-36L |
| Brand | KOBELCO |
| Electrode Type | Welding Electrodes for Stainless Steel |
| Welding Electrode Size | 2.0mm, 2.6mm, 3.2mm, 4.0mm and 5.0mm |
| Welding Process | SMAW |
| Weight Per Packaging | 20 Kg |
| Polarity | AC, DCEP |
| AWS Standard | AWS A5.4 E316L-16 |
| Re-Drying Conditions | 150–200°C for 0.5–1 hour |
| Identification Color | Green (first layer) |
Mechanical properties of all metals being welded
| Parameters | Typical Value (AC) | Collateral Value |
|---|---|---|
| Yield Strength | 420 MPa | – |
| Tensile Strength | 580 MPa | Minimum 483 MPa |
| Elongation | 45% | Minimum 30% |
| Impact Value (0°C) | 83 J | – |
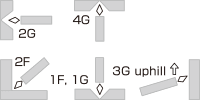
The KOBELCO NC-36L welding electrode can be used in various welding positions, offering flexibility for stainless steel fabrication, construction, and maintenance work.
Recommended Production Size and Welding Current
| Ø (mm) | 1F, 1G, 2F, 2G (A) | 3G Up, 4G (A) |
|---|---|---|
| 2.0 | 50–75 | 45–65 |
| 2.6 | 75–95 | 70–90 |
| 3.2 | 85–120 | 80–115 |
| 4.0 | 110–160 | 90–140 |
| 5.0 | 150–200 | – |
Chemical composition of all welded metals (mass %)
| Element | Typical Value (AC) (%) | Collateral Value (%) |
|---|---|---|
| C | 0.03 | Max. 0.04 |
| Si | 0.36 | Max. 1.00 |
| Mn | 1.50 | 0.50–2.50 |
| P | 0.03 | Max. 0.04 |
| S | <0.01 | Max. 0.03 |
| Ni | 12.0 | 11.0–14.0 |
| Cr | 19.4 | 17.0–20.0 |
| Mo | 2.2 | 2.0–3.0 |
| Cu | 0.11 | Max. 0.75 |
Note: The single value in the Guarantee Value column indicates the maximum limit.
| Ø (mm) | Length (mm) | kg/pack | kg/carton | g/stick | Carton Size (mm) |
|---|---|---|---|---|---|
| 2.0 | 250 | 2 | 20 | 11 | 300W × 130H × 280L |
| 2.6 | 300 | 2 | 20 | 20 | 300W × 100H × 330L |
| 3.2 | 350 | 5 | 20 | 36 | 175W × 110H × 380L |
| 4.0 | 350 | 5 | 20 | 55 | 175W × 115H × 380L |
| 5.0 | 350 | 5 | 20 | 82 | 175W × 115H × 380L |
Order NC-36L welding electrode now via WhatsApp for consultation and the best offer.
ISO 9001:2015
ISO 14001:2015
© 2026, PT. Intan Pertiwi Industri | All Rights Reserved.